Three routes, and you only need one of them
Quality work starts from one of three positions. Find yours and take the links in that card; the other two will not be useful to you yet.
- 32 engineering articles on this page, each answering one question
- Covering defect classes, AOI and AQL inspection, qualification testing and certification
- Every article linked at the point where you would need it
Something is wrong with the display
A unit has a fault and the first question is what it is called, because the name decides whether it is a defect, a wear mechanism, or damage that happened after delivery.
- Black spots: defect classes and where they come from
- Dead, stuck and bright pixels: definitions and limits
- ISO 9241-307 pixel-defect classes
- Streaks and line defects: source and detection
- Pressure marks: mechanism and AQL treatment
- Mura and luminance uniformity
- Burn-in versus image retention
- Yellowing and panel ageing
- Liquid ingress: failure signatures
- Production defects versus field damage
Inspect and qualify it
The order is placed and the work is proving that what arrives matches what was specified, and that the design survives the environment it was bought for.
- Incoming inspection: what to check and how often
- What to test when LCDs arrive
- How AQL inspection works on an LCD order
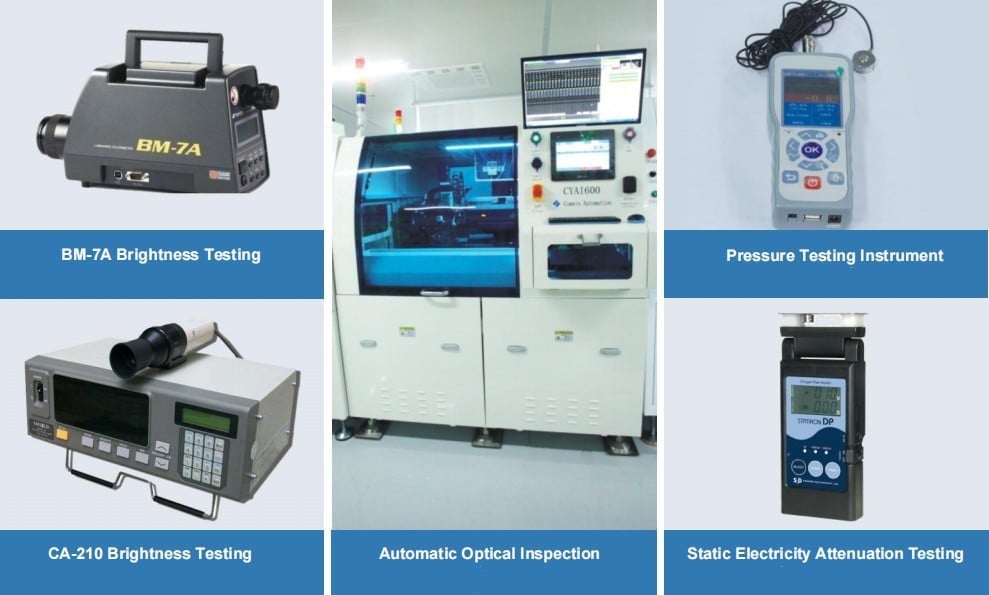
- How AOI detects defects
- How AOI delivers zero-defect shipments
- Building a qualification test plan
- Thermal cycling, humidity and altitude testing
- Vibration and shock testing
- How reliability is validated through testing
- How ESD protection improves reliability
Certify it and document it
The product is going to market and the questions are now regulatory: which certificates apply, what has to be filed, and what you can still change afterwards.
- Which certifications actually matter for your market
- Which factory certifications matter
- IEC 62368-1 for display-based equipment
- EMC certification: passing the first time
- RoHS, REACH and conflict-minerals documentation
- IP ratings explained
- Thermal design for sealed enclosures
- RMA and 8D field failure analysis
- Second-source qualification without doubling inventory
- Specification terminology buyers confuse
Who you are buying from decides what you can prove
Two articles sit behind every quality argument: how the factory was chosen, and whether the design can survive the transition into volume.
Choosing a factory is a verification exercise
A certificate is evidence that a type test passed, not that the goods in the container match the tested article. What closes that gap is process evidence: incoming checks, in-process inspection, final AQL and batch records that survive an audit.
The prototype-to-volume gap is where quality is won
Most quality problems are decided between the approved sample and the first production shipment, when tooling, process windows and inspection limits are fixed. Getting that transition documented is what makes the volume build repeatable.
What actually decides whether quality holds
Four things decide the outcome, and none of them is the pass rate on the final inspection.
The acceptance standard, agreed before the order
Most disputes about defects are really disputes about the limit. A pixel specification, a mura limit and an AQL level agreed in writing turn an argument into a measurement.
Inspection at the right point in the process
Final inspection finds problems; in-process inspection prevents them. A batch record that shows where a fault was caught is also what answers an audit two years later.
The environment test, not the datasheet rating
A module rated to a temperature survives that temperature on a bench. Whether the assembly survives it inside the enclosure, at the mounting angle, with the heat path the product actually has, is a separate test.
Change control after approval
A display programme runs for years. What protects it is notification of material, process and firmware changes, and a documented route back to requalification.
Where to go from here
If your question is not really about quality, one of these is closer to it.
Display quality questions
The five questions that arrive most often when a display order is inspected or rejected.
How many dead pixels are acceptable?
What is the difference between AQL and 100 % inspection?
What does a qualification test plan have to contain?
Do we need our own test reports or can we use the supplier’s certificate?
When should a second source be qualified?
Send us your display requirement
Tell us the product, the market you sell into, the environment it runs in and the defect standard you work to. We will come back with the test plan and documentation that market requires, and the batch records to go with each shipment.
Request a quality review