Second-Source Qualification for Display Modules Without Doubling Your Inventory Risk
Differentiation page: publish the linked new page before the foundation rewrite of the old page. | Meta description: Second-source qualification for display modules: interchangeability levels, the evidence set, keeping the source alive and avoiding…
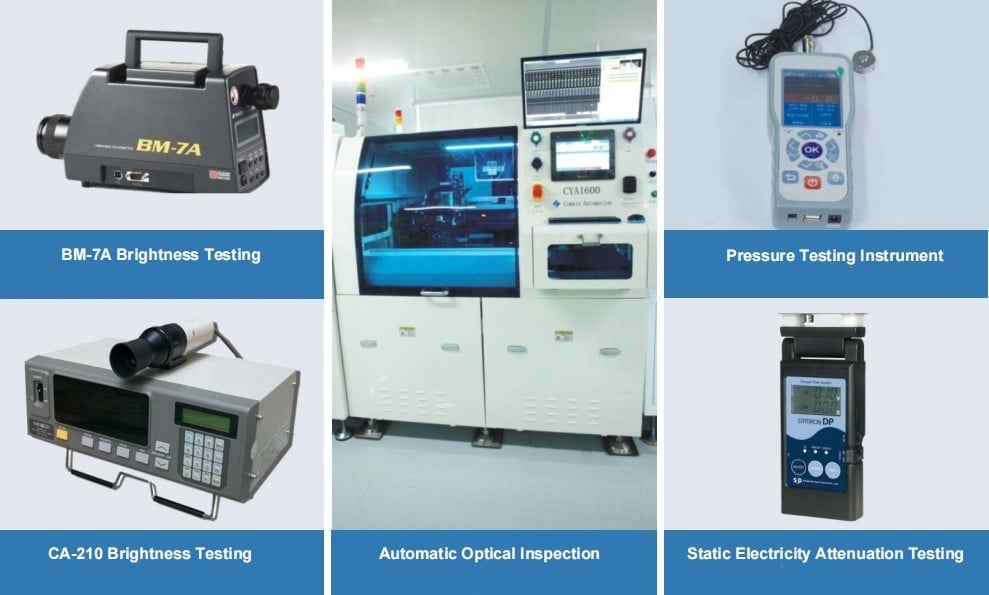
Second sourcing is usually framed as insurance, and insurance has a premium. For displays, the premium is qualification cost, duplicated inventory and the maintenance effort required to keep the alternate source genuinely usable. A second source that has not been built for two years is a drawing, not a fallback. The useful question is how much premium buys how much protection.
Part of the Quality, Testing & Compliance guide — 33 articles on defect classes, inspection, qualification and certification.
What a second source can and cannot protect against
It protects against supply interruption, not against design change.
A qualified second source addresses a supplier’s inability to deliver: capacity constraints, a plant issue, a commercial dispute, or a discontinued component. It does not protect against a change that affects the product’s performance, because both sources have to satisfy the same specification, and it does not remove the need for change notification. Where the risk is a panel reaching end of life, a second source is useful only if it uses a different panel family – which makes it a different design, not an alternate supplier.
Clarifying which risk is being addressed determines whether the effort should go into a second supplier, a service stock, or a documented retrofit path.
Interchangeability levels, revisited
The level determines the cost of switching.
| Level | What differs | Switching cost |
|---|---|---|
| Drop-in | Nothing, within drawing tolerances | Incoming inspection only |
| Form-fit-function | Firmware, timing or minor mechanics | Firmware change and verification |
| Requires adaptation | Bracket, cable, connector or interface | Mechanical change plus validation |
| Requires redesign | Panel family, resolution or interface generation | A new programme |
Only the first level delivers the insurance most buyers imagine. The second is usually acceptable if the firmware path is maintained. The third and fourth are better described as contingency plans than as second sources.
The evidence set a second source must provide
The same evidence as the primary, verified independently.
- Product specification with tolerances and test methods.
- Optical measurements: luminance, uniformity, colour and contrast in defined conditions.
- Environmental results at the same conditions as the primary source.
- Mechanical drawings compared against the primary, dimension by dimension.
- Material declarations for the front assembly and the electronics.
- Traceability example and change notification commitment.
The comparison should be a document rather than an assumption: a table showing each characteristic, the primary source’s value, the second source’s value, and the difference. That table is what allows a switching decision to be made quickly, and it is also the evidence a customer may request if the product’s approval depends on the display. Certificate scope for both sources should be verified through an accreditation register, as described by the International Accreditation Forum.
Keeping the source alive
An unused qualification decays.
Processes, materials and firmware change at both sources over time, and a second source that is not exercised drifts out of alignment with the approved configuration. The practical maintenance is an annual build of a small quantity, verified against the comparison table, with the results recorded. That annual exercise costs a fraction of a full requalification and keeps the switching option real. Workmanship expectations for the assemblies compared are published by bodies such as IPC.
Where the second source’s product changes in a way that would require revalidation, the change notification agreement is what surfaces it in time to decide whether to keep the qualification or accept the loss of the option.
Inventory strategy without doubling risk
Two sources, one of which is idle, is not free.
Holding stock from two sources doubles the inventory exposure to obsolescence and to engineering changes, and it complicates traceability because two material streams converge on the same product. The alternatives are to hold a service stock from the primary source only and keep the second source qualified but unstocked, or to run the second source at a low but regular share of production so that it remains a live process. The second approach is often better where the product’s volume supports it, because it keeps both processes in practice rather than in theory.
Where the display is part of a regulated product, the inventory decision also has a documentation dimension: units from a second source should be identifiable in traceability records so that a field investigation can distinguish them.
Cost of maintaining a second source
Four cost elements, all predictable.
| Element | Driver | How to limit it |
|---|---|---|
| Initial qualification | Testing and documentation effort | Reuse the primary source’s test plan and limits |
| Recurring verification | Annual or semi-annual build and test | Small sample, focused on the characteristics that differ |
| Inventory | Stock held from two sources | Stock one source; qualify the other without stocking |
| Engineering change | Two sets of notifications to process | Require identical change notification commitments |
Framed this way, the question becomes whether the protection is worth those four costs, which is a business decision rather than a technical one. The technical contribution is to make the costs explicit and to keep the switching path documented.
When a second source is not the right answer
Four cases where the effort is better spent elsewhere.
- The panel family is unique and no alternate produces a compatible format; a retrofit path is more useful.
- The product volume is low and a service stock is sufficient protection.
- The display is a small share of the product’s cost, so the risk is better accepted than managed.
- The qualification would require a change to the product’s approval, making the alternate unusable without re-certification.
In these cases, the practical protections are a service stock, a documented retrofit path and a change notification agreement – all cheaper than a second source that cannot actually be switched to.
A switching procedure that works under pressure
Write the procedure before it is needed.
- Confirm the second source’s current verification data is within date.
- Verify the specific lots offered against the comparison table.
- Check the mechanical and firmware differences and apply the planned adaptation.
- Run the defined acceptance tests on the first shipment, at a higher sample rate than normal.
- Identify the units in traceability records and notify any affected customer or regulator.
- Record the switch, the verification and any deviation found.
A procedure like this turns a supply emergency into a planned transition, which is the actual benefit of second sourcing. CDTech’s notes on second-source qualification describe the underlying evidence set, and the same documentation supports both sources equally.
FAQ
How do I qualify a second display supplier?
Require the same specification, optical, environmental and material evidence as the primary source, and compare the two in a document rather than by assumption. Then build and verify a small quantity periodically so the qualification does not decay, and keep a switching procedure ready.
Does a second source protect against a panel reaching end of life?
Only if the second source uses a different panel family and interface, which makes it a different design rather than an alternate supplier. For end-of-life risk, a service stock and a documented retrofit path are usually more effective than a second source using the same panel.
How often should a second source be built?
Periodically enough that the process stays aligned with the approved configuration – annually for many products – with a small sample verified against the comparison table. An unexercised qualification is not a fallback, because processes and materials change at both sources over time.
Should stock be held from both sources?
Holding stock from both doubles the exposure to obsolescence and complicates traceability. A common approach is to stock the primary source and keep the second qualified but unstocked, or to run the second source at a small but regular share of production so both processes remain live.
What should a switching procedure contain?
A check that the second source’s verification data is current, lot-level verification against the comparison table, the planned mechanical or firmware adaptation, an elevated acceptance test on the first shipment, identification of the units in traceability records and a record of the switch and any deviation found.
Next step
Send the module specification, volume profile and continuity requirements to CDTech; the reply will document the achievable interchangeability level and the evidence set for a second source.
Contact sales@cdtech-lcd.com or use the contact page.
Related articles
 Incoming Inspection for Display Modules: What to Check and How OftenQuality, Testing & ComplianceEMC Certification for Display Products: Passing the First TimeQuality, Testing & ComplianceScreen Damage Modes: Distinguishing Production Defects From Field DamageQuality, Testing & ComplianceScreen Streaks and Line Defects: Source and DetectionQuality, Testing & Compliance