ISO 9241-307 Pixel-Defect Classes Explained for Buyers and QC
Pixel-defect arguments are almost never about whether a defect exists. They are about whether the defect was within the accepted class - and that depends on a standard, a counting rule and a viewing…
Pixel-defect arguments are almost never about whether a defect exists. They are about whether the defect was within the accepted class – and that depends on a standard, a counting rule and a viewing condition that were usually never written down.
Part of the Quality, Testing & Compliance guide — 33 articles on defect classes, inspection, qualification and certification.
This article explains what the classes define, how they scale with resolution, and how to turn a class into an inspection clause that both sides can apply the same way.
What the defect classes actually define
The pixel-defect classes describe limits for defective picture elements and sub-pixels on a display, expressed as counts per million pixels and differentiated by defect type and severity. They are written to allow a display to be manufactured and sold within a stated quality level rather than to guarantee a perfect panel.
The key point for buyers is that the class is a limit, not a promise about any individual unit. Two panels from the same production lot can differ: one with no visible defects, one with the maximum count the class permits. Both are conforming.
Defect types you will see
Four types cover most real cases. Bright defects appear as illuminated dots on a dark background. Dark defects appear as black dots on a white background. Partial defects affect a sub-pixel, producing a colour fringe rather than a full dot. Clustered defects are two or more adjacent defective pixels, and they are treated more severely because the eye notices them more readily than isolated dots.
Defect type matters as much as count. A single bright defect in the centre of a screen is far more visible than several dark defects near an edge, which is why classes differentiate by type and why a fair clause states where defects are counted and how clusters are treated.
How limits scale with resolution
Because limits are expressed per million pixels, the permitted count rises with resolution. A 10.1-inch WXGA panel and a 1080p panel of the same size can both conform to the same class while allowing different numbers of defects.
This produces two counter-intuitive results. Higher-resolution panels are not automatically “cleaner”. And a supplier quoting “zero defects” for a high-resolution panel is usually describing a marketing position rather than a manufacturing reality – or quoting a much stricter class that carries a cost.
Why zero-defect expectations backfire
Applications differ, and the clause should reflect that. A screen viewed at two metres in a control room and a screen examined at 40 cm by an inspector have different thresholds for what counts as visible. Writing one clause for both, and applying it at the stricter distance, wastes good panels; applying it at the looser distance lets visible defects through on the product that needs them least.
Applications differ, and the clause should reflect that. A screen viewed at two metres in a control room and a screen examined at 40 cm by an inspector have different thresholds for what counts as visible. Writing one clause for both, and applying it at the stricter distance, wastes good panels; applying it at the looser distance lets visible defects through on the product that needs them least.
Demanding zero defects has three consequences. The supplier either refuses, prices defensively to cover the reject rate, or accepts and then argues at inspection about whether each dot is a defect.
In practice, a written defect class with a clear counting rule produces better outcomes than an absolute demand, because it converts a disagreement about judgement into a measurement. If your application genuinely cannot tolerate a single visible defect – an imaging device, or a screen the operator looks at from 30 cm all day – then say so explicitly, accept the cost, and define the inspection method with the same precision.
Turning a class into an inspection clause
A usable clause has five elements: the class or limit, the defect types covered, the background and grey levels used for inspection, the viewing distance and time, and the counting rule including how clusters are handled.
| Element | What to write |
|---|---|
| Limit | Class plus counts by defect type, or a project-specific table |
| Defect types | Bright, dark, partial, clustered – with cluster rules stated |
| Test patterns | Full white, full black and the primary colours |
| Viewing condition | Distance, angle, illumination and inspection time |
| Counting rule | How to count sub-pixel defects, and whether defects are counted in the central zone separately |
Sampling and viewing conditions
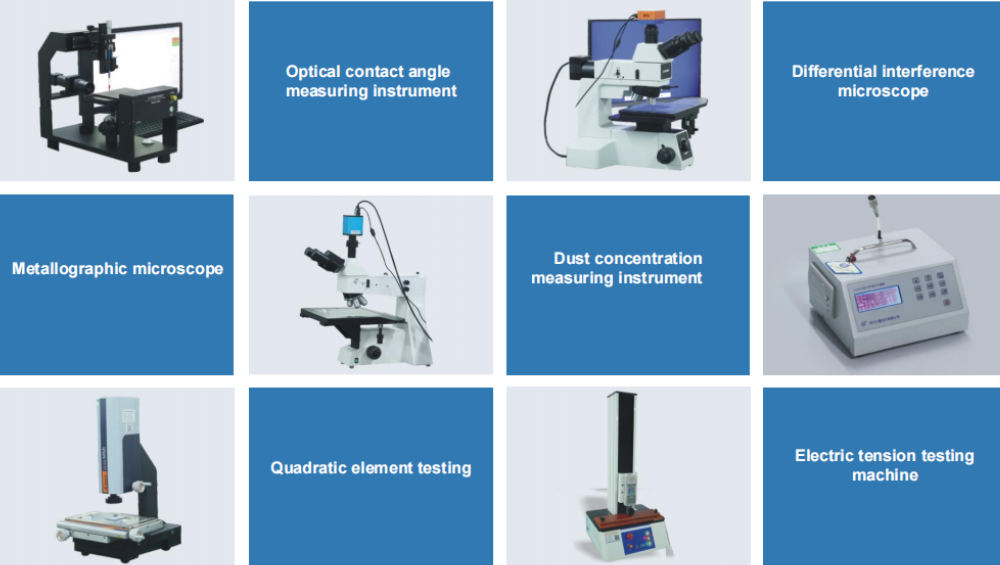
Defect counts are only reproducible when the viewing conditions are fixed. Inspection at 30 cm under bright overhead light finds defects that inspection at 60 cm in a dim room does not.
Write down an inspection distance related to the real use case – not to the inspector’s comfort – and a maximum inspection time per unit. Inspection with no time limit will always find more, which makes acceptance impossible to reproduce between shifts or sites. Standardising the condition is what makes the clause usable rather than theoretical.
Recording defects so claims work
Incoming inspection and pixel-defect counting are the same discipline applied at different points: the sampling rule in AQL inspection for LCD orders explains how many units to check and how to record the result.
A worked record looks like this: unit serial, production week, test pattern (full white, 50 per cent grey, full black, red, green, blue), viewing distance of 50 cm, room illumination of 300 lux, inspection time of 30 seconds per pattern, and a defect table listing each bright or dark element with its screen position and whether it participates in a cluster. Signed and dated by the inspector. That record is comparable across shifts, and it survives a disagreement because it describes the test rather than the opinion.
A claim needs evidence that the defect is in the panel and not the result of handling. Record the unit serial number, the defect position as coordinates or as a marked photograph, the test pattern used, the viewing distance and the inspection result.
Photographs taken through the inspection instrument are more convincing than those taken with a phone, because they show the conditions as well as the defect. Whatever method you use, apply it consistently so that two inspectors produce comparable records.
Specification versus marketing claim
“Zero pixel defects” in marketing material is not a specification you can inspect against. Treat it as a claim requiring definition: ask which class applies, what the counting rule is, and whether the promise survives at the agreed inspection distance.
If the answer is a stricter class than the standard default, ask for it in writing with the inspection method. The same discipline applies to every parameter on the sheet, which is why reading an LCD datasheet is worth doing with the counting and measurement rules in view. That is a specification. Everything else is positioning.
Negotiating a workable limit
Cost behaves predictably here. Tightening the limit across the whole screen raises the supplier’s reject rate, and the reject rate is passed back in price. Tightening only the central area – the zone the operator actually reads – raises the reject rate much less, because edge defects are common and central defects are not. That asymmetry is what makes a zoned specification the cheapest way to protect the part of the screen that matters.
The most useful negotiation is not about the count. It is about the central zone. Buyers often care far more about where defects appear than how many exist, because a defect in the middle of an interface is visible and one at the edge may never be noticed.
Agreeing a stricter limit for the central area and a standard limit elsewhere frequently costs less than a uniform tightening and matches how the product is actually used. It also gives the supplier a practical specification to build to.
Acceptance-clause checklist
| Question | Acceptable answer |
|---|---|
| Which class or limit applies? | Named class, or a project table by defect type |
| How are clusters counted? | Explicit rule, not left to judgement |
| What background and patterns? | Listed, with grey levels |
| From where and for how long? | Distance, angle, illumination and inspection time |
| Is the central zone different? | Stated separately if the application needs it |
| How are results recorded? | Serial, position, pattern, conditions, evidence |
Bringing this clause to the first sample inspection – rather than to the first dispute – removes most of the argument before it starts.
Frequently asked questions
Does a defect class guarantee no visible defects?
No. It defines a limit that a conforming unit may reach. A unit with defects up to that limit is still conforming.
Can we require zero defects?
You can require it, but expect either a refusal, a price that covers the reject rate, or a dispute at every inspection. A stricter class with a defined method is usually more workable.
Do we need a microscope to inspect pixel defects?
Usually not. Human inspection at a defined distance with the standard patterns is the normal method; magnification is used for analysis, not for routine acceptance.
Where a defect appears in service, the class matters as much as the count: a dark sub-pixel in a corner and a bright cluster in the centre of an image are different problems. Recording the class and the position at receiving keeps that distinction available later.
Related articles
 Second-Source Qualification for Display Modules Without Doubling Your Inventory RiskQuality, Testing & Compliance
 Incoming Inspection for Display Modules: What to Check and How OftenQuality, Testing & ComplianceEMC Certification for Display Products: Passing the First TimeQuality, Testing & Compliance
 Screen Damage Modes: Distinguishing Production Defects From Field DamageQuality, Testing & Compliance