Mura and Luminance Uniformity: Causes, Detection and Acceptance
Mura is the display industry's word for unevenness: patches, streaks or blotches that break the uniformity of an otherwise correct image. It is the most common quality dispute in display supply, and the hardest…
Mura is the display industry’s word for unevenness: patches, streaks or blotches that break the uniformity of an otherwise correct image. It is the most common quality dispute in display supply, and the hardest to resolve, because the complaint is subjective until someone defines the conditions under which it is measured.
This article separates appearance from cause, which is what turns a dispute into a corrective action.
What is mura and what is not
Mura describes a local variation in luminance, colour or both, visible as a patch or streak rather than as a single defective pixel. It differs from a pixel defect, which is discrete, and from a viewing-angle effect, which changes with the observer’s position rather than staying with the panel.
That distinction decides who owns the problem. A discrete defect is a component failure; mura is usually a manufacturing, assembly or mechanical issue, and often the assembly part is the customer’s own mechanical design.
Describing appearance so others can verify it
Descriptions such as “cloudy” or “uneven” cannot be verified. A usable description includes the background grey level, the position of the artefact relative to the panel edge, its approximate extent as a fraction of the screen, whether it changes with viewing angle, and whether it is visible with the panel switched off under reflected light.
The last point is more diagnostic than it looks: an artefact visible with the power off is usually a surface or bonding phenomenon rather than an electrical one.
Panel-level causes
The first question in any mura investigation is whether the artefact was present before assembly. That is worth checking systematically rather than by impression: inspect a bare panel from the same lot, at the same grey levels, before it is bonded or mounted. If the pattern is already there, everything downstream is a distraction.
The first question in any mura investigation is whether the artefact was present before assembly. That is worth checking systematically rather than by impression: inspect a bare panel from the same lot, at the same grey levels, before it is bonded or mounted. If the pattern is already there, everything downstream is a distraction.
Some mura originates in the panel itself: cell-gap variation, alignment irregularities, or transistor uniformity across a large area. These appear as broad, soft patterns, usually with a gradual transition, and are stable over time because they are built into the panel.
They are also the hardest to correct downstream. If a pattern is present on a bare panel before bonding and before any mechanical assembly, the conclusion is usually a panel-level yield issue, and the response is a claim rather than a design change.
Bonding-related artefacts
Optical bonding introduces its own signature. Trapped particles and voids produce localised bright or dark spots with relatively sharp edges. Uneven adhesive thickness produces broader patches. Delamination shows as an edge-origin artefact that grows with temperature or time.
The bonding method itself changes the risk: a comparison of OCA and OCR bonding explains why the two processes fail differently. Bonding-related artefacts usually appear after the panel has been bonded and change with temperature, which is a useful differentiator: a pattern that intensifies in a warm enclosure is more likely to be an adhesive or mechanical phenomenon than a panel defect.
Backlight and light-guide contributions
Backlight patterns also have a thermal signature. Light-guide warping and diffuser expansion change with temperature, so a pattern that shifts or softens after twenty minutes of operation is more likely to be backlight-related than panel-related. Record the observation at switch-on and again after thermal equilibrium; the difference between those two states is one of the most useful pieces of evidence in a uniformity report.
Backlight patterns also have a thermal signature. Light-guide warping and diffuser expansion change with temperature, so a pattern that shifts or softens after twenty minutes of operation is more likely to be backlight-related than panel-related. Record the observation at switch-on and again after thermal equilibrium; the difference between those two states is one of the most useful pieces of evidence in a uniformity report.
Backlight assemblies produce their own uniformity patterns. Insufficient mixing distance creates brighter regions near the LEDs, and light-guide or diffuser irregularities appear as streaks or as a directional gradient.
The distinguishing feature is behaviour with grey level. Backlight-driven patterns are usually most visible on mid-grey fields and less obvious on full white, while panel-driven patterns often behave the other way around. Testing at several grey levels therefore separates the two families before any disassembly.
Mechanical stress and mounting pressure
The diagnostic sequence is straightforward and takes minutes. Inspect the assembly as built; then loosen the fasteners progressively and inspect at each step; then remove the module from the enclosure and inspect it on the bench. If the pattern weakens as the fasteners are loosened and disappears on the bench, the enclosure is the cause and no panel claim will change anything. If it remains, the cause is in the module and the investigation moves to bonding, backlight or panel.
The most under-diagnosed cause is the one the customer owns: mechanical stress. A screw tightened against the panel edge, a bracket that does not follow the housing’s flatness, or a gasket compressed beyond its design range all introduce local pressure, and local pressure changes the cell gap, which shows up as mura.
The signature is a pattern aligned with the mounting points or with the frame, appearing after assembly and often disappearing when the module is removed. If it behaves that way, stop looking at the panel and look at the mechanical design.
Detection conditions and grey-level patterns
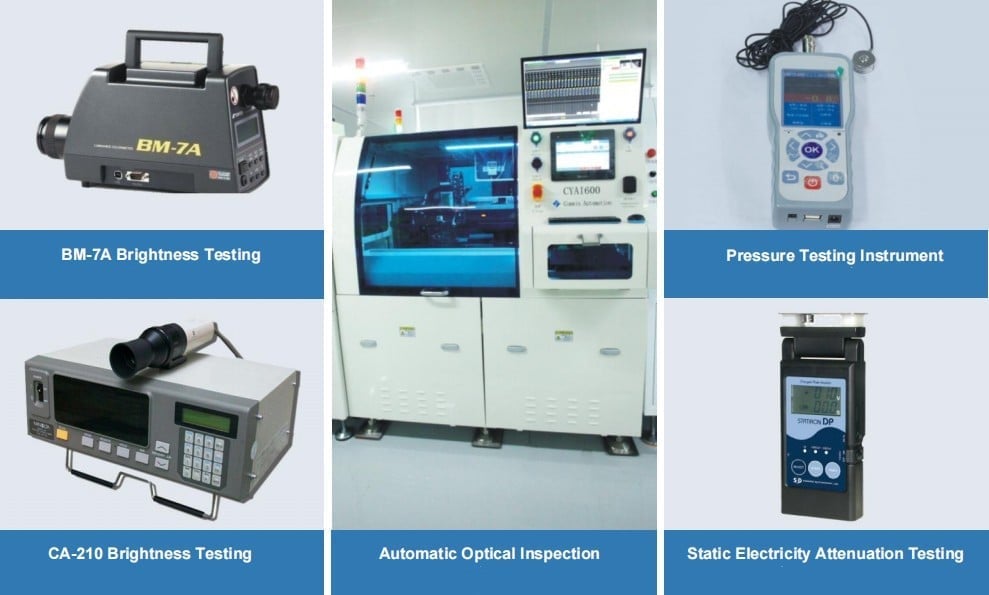
Visual inspection and instrument measurement find different things. The eye is better at detecting a soft, broad pattern on a mid-grey field; an imaging colorimeter is better at quantifying a subtle gradient that the eye tolerates. Where a dispute is likely, run both: the measurement establishes the magnitude and the photograph shows what a person actually sees. Neither alone is sufficient, because a measurement without a photograph can be dismissed as academic and a photograph without a measurement can be dismissed as an artefact of the camera.
Uniformity defects are invisible on some content and obvious on others. Full white hides backlight patterns; mid-grey exposes them. Full black hides almost everything except bright artefacts. Red, green and blue fields expose colour-specific unevenness.
Where the artefact is a manufacturing pattern rather than an assembly effect, detection methods overlap with those used in automated optical inspection. A workable detection routine shows at least full white, 50 per cent grey and full black, from the normal viewing distance, after the panel has reached thermal equilibrium, in a defined ambient light. Anything less will produce results that cannot be reproduced.
Recording evidence that survives a dispute
Photographs taken at the wrong exposure prove nothing, because a phone camera adjusts to make the screen look even. Record instead: the test pattern, the camera settings or instrument used, the viewing distance, the lighting condition, and the same view taken from two angles.
Where the artefact is subtle, an imaging colorimeter measurement is far more persuasive than a photograph, because it produces a number and a map rather than an impression. Even a simple luminance map across nine points distinguishes a broad gradient from a local defect.
Acceptance approaches that actually work
Whichever approach is used, apply it at a fixed point in the process. Inspecting some units after bonding and others after mechanical assembly makes the data incomparable, because the two states have different stress histories. Choose one inspection point, name it in the specification, and keep it constant even when the process changes.
Whichever approach is used, apply it at a fixed point in the process. Inspecting some units after bonding and others after mechanical assembly makes the data incomparable, because the two states have different stress histories. Choose one inspection point, name it in the specification, and keep it constant even when the process changes.
Absolute uniformity requirements are expensive and hard to verify. Two approaches work better in practice.
The first is a measurement-based limit: a maximum deviation between the centre and the sampling points, measured under stated conditions. It converts the argument into arithmetic. The second is a reference-sample approach: both sides agree on an approved unit, and the acceptance decision is a comparison against it. The reference sample needs to be stored properly and re-agreed when either side changes supplier or process.
Mura report template
Include one further field in the report: what was done to the unit before the observation. A pattern seen on a bare panel and the same pattern seen after two thermal cycles are different events with different consequences, and the report should make that distinction impossible to miss.
Include one further field in the report: what was done to the unit before the observation. A pattern seen on a bare panel and the same pattern seen after two thermal cycles are different events with different consequences, and the report should make that distinction impossible to miss.
| Field | Why it is needed |
|---|---|
| Serial and production lot | Establishes whether the pattern is isolated or systematic |
| Test pattern and grey level | Defects appear differently at different levels |
| Ambient light and viewing distance | Makes the observation reproducible |
| Appearance description and position | Allows the cause family to be narrowed |
| Behaviour with temperature | Separates bonding and mechanical causes from panel causes |
| Behaviour with the power off | Separates surface and bonding artefacts from electrical ones |
| Assembly state | Shows whether the artefact follows the mounting |
| Evidence | Measurement map or controlled photograph |
If a uniformity problem is showing up in your assemblies, send us the pattern description, the grey level and the assembly state – those three answers usually identify the cause family before any parts travel.
Frequently asked questions
Is mura a defect or a normal variation?
Both, depending on the acceptance criteria. Panels within a stated uniformity limit are conforming even if a pattern is visible. The problem is not the pattern but the absence of an agreed limit.
Can mura appear after the panel has been in service for a while?
Yes, particularly when it is mechanical or bonding-related and the assembly experiences temperature cycles. That is one reason to record the initial condition of a new assembly.
Should we reject a sample with a visible pattern?
First establish whether the pattern survives with the module removed from your assembly. If it disappears, the panel is not the cause.



