Haze, Gloss and Surface Treatment: Measuring Cover-Glass Optics
Two numbers describe most of what a front surface does to light: haze and gloss. They are related but not interchangeable, and they can be traded against each other freely in the coating specification…
Two numbers describe most of what a front surface does to light: haze and gloss. They are related but not interchangeable, and they can be traded against each other freely in the coating specification – which is why two suppliers can both offer “anti-glare” and deliver visibly different products.
This article explains what the numbers mean, which lighting condition each treatment addresses, and how to write a surface specification that can actually be verified.
What haze and gloss actually describe
Gloss describes how much light reflects from the surface in the mirror direction. A polished surface produces a strong, sharply defined reflection; a rougher surface spreads that reflection out and appears less glossy.
Haze describes the proportion of transmitted light that is scattered rather than passing straight through. In display terms, higher haze means images look slightly veiled, particularly on high-contrast content.
The two are measured in different geometries and expressed in different units, and neither alone predicts readability. A surface can be low-gloss and low-haze, or high-haze and still glossy – which is why the specification needs both numbers rather than a treatment name.
How each treatment changes the surface
Anti-glare treatments work by creating a controlled surface texture. The texture scatters the reflected image across a wider angle, so the reflection’s intensity at any one point drops. The cost is haze: the same texture scatters transmitted light, softening the image very slightly.
Anti-reflective coatings work differently. Instead of scattering the reflection, they reduce it using thin-film interference, so the reflection is weaker without the image being veiled. The trade-offs are cost, durability and a surface that shows fingerprints and cleaning marks more readily.
Some products combine both: a lightly textured base with an anti-reflective coating on top. That combination can be effective, but the two contributions need to be specified separately or the measurement becomes ambiguous.
Measurement geometry and instruments
Calibration status matters as much as geometry. Gloss and haze instruments drift, and a comparison between two surfaces measured on instruments calibrated at different times is weaker than it looks. Record the instrument and its calibration date with every measurement, exactly as you would for luminance work, so the numbers can be defended later.
Calibration status matters as much as geometry. Gloss and haze instruments drift, and a comparison between two surfaces measured on instruments calibrated at different times is weaker than it looks. Record the instrument and its calibration date with every measurement, exactly as you would for luminance work, so the numbers can be defended later.
Calibration status matters as much as geometry. Gloss and haze instruments drift, and a comparison between two surfaces measured on instruments calibrated at different times is weaker than it looks. Record the instrument and its calibration date with every measurement, exactly as you would for luminance work, so the numbers can be defended later.
Calibration status matters as much as geometry. Gloss and haze instruments drift, and a comparison between two surfaces measured on instruments calibrated at different times is weaker than it looks. Record the instrument and its calibration date with every measurement, exactly as you would for luminance work, so the numbers can be defended later.
Gloss is measured at a defined angle – commonly 20¡ã, 60¡ã or 85¡ã – and the choice of angle changes the result. A surface that reads glossy at 20¡ã may read matte at 85¡ã, because the texture scatters differently depending on the incidence angle.
Haze is measured in transmission, with an instrument that captures both the directly transmitted and the scattered light. The measurement must state the illumination and the acceptance angle, because a wider aperture collects more scattered light and reports higher haze.
Two rules make results comparable: fix the instrument geometry and state it with every number, and measure the same stack. A coating measured on bare glass and the same coating measured after bonding to a panel will not give the same figure, because the adhesive and the panel change the internal reflections.
Matching treatment to lighting condition
The right treatment follows from where the display is used.
| Lighting condition | Treatment that helps | Cost of choosing it |
|---|---|---|
| Direct sun or a strong directional source in the operator’s line of sight | Anti-glare texture, possibly with anti-reflective coating | Slight haze, visible on fine text |
| Bright but diffuse light from a wide area | Anti-reflective coating | Fingerprints and cleaning marks more visible |
| Dim indoor rooms, dark interfaces | Minimal treatment; clarity matters more than reflection | Reflections acceptable in controlled lighting |
| Mixed: indoor use with occasional window light | Light texture or no treatment | Either extreme is over-specified |
Contrast, clarity and the trade-offs
The trade-off between readability and clarity is real and should be decided with the product’s content in mind. On large text and graphics, haze is barely noticeable. On fine data, small fonts or detailed imagery, the same haze is a visible degradation.
The other trade-off is between reflection control and cleaning. A textured surface hides fingerprints better than a smooth anti-reflective coating, which matters on touch products used by many people. A smooth surface cleans more easily but shows every mark until it is cleaned.
Fingerprints, cleaning and wear
The glass itself is part of the same specification, and cover glass design covers how thickness, shape and treatment interact. Surface treatments change over a product’s life. Repeated cleaning gradually polishes a textured surface, reducing haze and increasing gloss; abrasive cleaners accelerate that process. Anti-reflective coatings can be damaged by the wrong solvent or by abrasion, and the damage appears as a patch of higher reflectance rather than as a visible scratch.
This is an argument for specifying the cleaning regime with the surface, and for checking what the glass looks like after the number of cleaning cycles the product will actually see.
Measuring bonded assemblies
Once the glass is bonded to the panel, the measurement describes the assembly, not the coating. Internal reflections between the glass and the panel change the transmitted and reflected light, and a bonded assembly usually measures differently from the same glass measured alone.
Choose one measurement state and use it consistently – either the bare glass or the finished assembly. Mixing the two produces numbers that cannot be compared, which is the most common cause of disputes about surface treatment.
Writing a verifiable surface specification
One further detail is worth stating explicitly: whether the treatment applies to one surface or both, and whether the specification covers the glass before or after any printing, coating or bonding step. Coatings applied before a bonding process can be affected by the process itself, and a specification that ignores the sequence measures the wrong article.
One further detail is worth stating explicitly: whether the treatment applies to one surface or both, and whether the specification covers the glass before or after any printing, coating or bonding step. Coatings applied before a bonding process can be affected by the process itself, and a specification that ignores the sequence measures the wrong article.
One further detail is worth stating explicitly: whether the treatment applies to one surface or both, and whether the specification covers the glass before or after any printing, coating or bonding step. Coatings applied before a bonding process can be affected by the process itself, and a specification that ignores the sequence measures the wrong article.
One further detail is worth stating explicitly: whether the treatment applies to one surface or both, and whether the specification covers the glass before or after any printing, coating or bonding step. Coatings applied before a bonding process can be affected by the process itself, and a specification that ignores the sequence measures the wrong article.
A usable specification names the treatment, gives gloss and haze values with their measurement geometry, states the measurement state (bare glass or bonded assembly), and defines the acceptance band rather than a single target.
It should also state the cleaning agents and methods the surface must tolerate, and whether the specification applies to the centre of the glass or the whole surface. Coatings applied by dipping or spraying can vary across a large piece, and the specification needs to say where the limits apply.
Incoming verification of treated glass
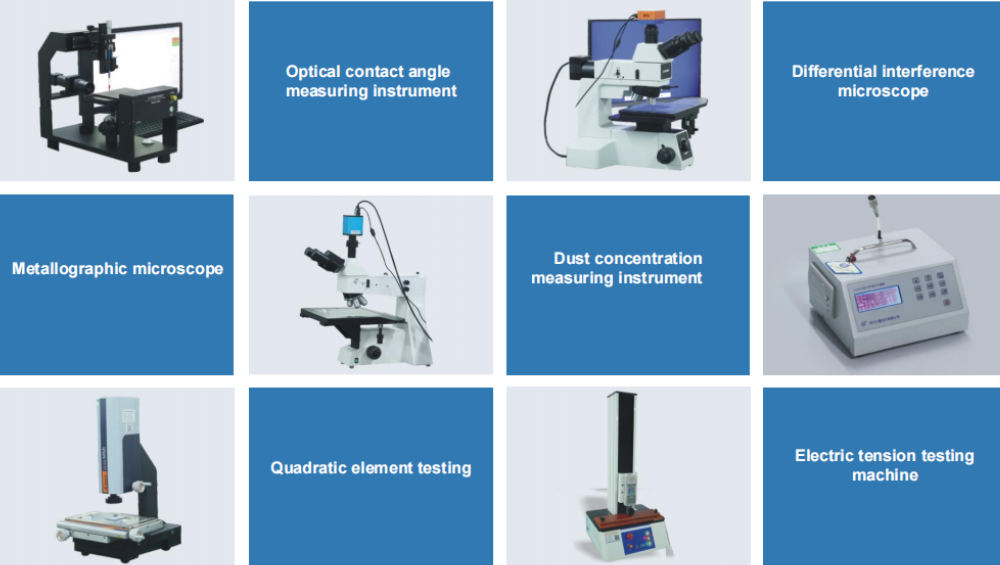
Incoming inspection does not need a full optical laboratory. A gloss meter at the specified angle, a haze measurement on the agreed instrument and a visual check under a defined light source will catch most supplier variation. What matters is doing the same test the same way every time, and recording the geometry with the value.
Where a batch is out of band, the record of geometry and measurement state is what makes the conversation with the supplier productive rather than circular.
Comparison pitfalls checklist
| Pitfall | Effect on the comparison |
|---|---|
| Comparing gloss values measured at different angles | Numbers are not comparable at all |
| Comparing haze with different aperture sizes | One supplier appears measurably better for no physical reason |
| Measuring bare glass against a bonded assembly | Internal reflections change the result |
| Using a treatment name instead of numbers | “Anti-glare” can mean anything within a supplier’s range |
| Specifying a single target instead of a band | Normal process variation becomes a non-conformance |
| Ignoring the cleaning regime | The surface that measured well when new degrades within a year |
If two suppliers are reporting different numbers for what should be the same surface, send us both specifications with their measurement geometry – the difference is usually in the conditions rather than the coating. For the coating technologies themselves, see the article on AG and AR glass coatings.
Frequently asked questions
Does higher haze make a display worse?
Not by itself. Higher haze reduces direct reflection, which improves readability in bright environments. It becomes a problem when the content is fine and the loss of clarity matters more than the reduction in reflection.
Can we specify “anti-glare” without numbers?
You can, but the result is unpredictable, because a single treatment name covers a range of textures. Specifying gloss and haze bands with their geometry is what makes the specification enforceable.
Should the surface be measured before or after bonding?
Either, provided the same state is used consistently. Most disputes come from comparing one supplier’s bare-glass figure with another’s bonded-assembly figure.