Black Spots on a Display: Defect Classes and Where They Come From
Black spots on a display: the defect classes behind them, which originate in the panel or in assembly, how they are detected and how to specify them. | Target URL: https://blog.cdtech-lcd.com/black-spots-on-a-display/
A black spot is not one defect. It is a family of failures that look similar on a screen and differ completely in mechanism, origin and consequence: a particle trapped during bonding, a cell-gap irregularity, a micro-leak that will grow, or contamination inside the backlight. The classification decides whether it is a supplier acceptance question, a design problem or a field failure – and the answers to “can it be removed” are different for each.
Part of the Quality, Testing & Compliance guide — 33 articles on defect classes, inspection, qualification and certification.
What counts as a black spot on a display?
It is a locally darker region that stays dark when the panel is driven white.
Display engineers separate three things that users call a black spot. A point defect is a small, sharply bounded spot at or near a pixel; an area defect is a larger patch that follows no pixel boundary; and a shadow or bruise is a diffuse darkening that changes with viewing angle or pressure. Each behaves differently under magnification, and each points at a different layer of the stack.
Because the visual symptom is similar, the first useful step in any investigation is to view the defect on a uniform white and a uniform grey field, at several angles, with and without pressure on the cover glass. That single routine separates a surface artefact from a cell defect from an assembly defect.
The four mechanisms that produce them
Particle inclusion, cell damage, micro-leak and backlight contamination.
A particle trapped between the display and the cover glass during optical bonding creates a local optical discontinuity that appears as a dark dot or patch, often with a faint halo under magnification. Cell damage – a localised irregularity in the gap between the two glass plates, or a deformed spacer – changes how the liquid crystal transmits light in that region and produces an area defect that follows the cell rather than the pixel grid.
A micro-leak is a breach in the edge seal that lets liquid crystal escape and air or moisture enter; it starts small and grows along the leak path. Backlight contamination – dust, adhesive or a damaged diffuser inside the backlight – produces a dark region that is visible with the panel on but disappears when it is off, which is the fastest way to tell it apart from a cell defect.
Which defects originate in the panel and which in module assembly?
The origin determines who can fix it and what evidence to ask for.
Panel-side origins are cell-gap irregularity, spacer defects, seal defects and polariser contamination that occurs before the panel leaves the panel maker. Module-side origins are particles introduced during lamination or bonding, mechanical damage during handling or clamping, contamination inside the backlight during assembly, and damage caused during final mounting or packing.
In practice, a buyer cannot determine the origin from the symptom alone, which is why the supplier’s failure analysis matters more than the defect’s appearance. A supplier that reports only “panel defect” without sectioning or inspecting the stack is not analysing; it is transferring the cost.
How a black spot grows, and why that matters to acceptance
Growing spots indicate a leak or mechanical stress; static spots usually indicate an inclusion.
A spot that enlarges over days or after thermal cycling is characteristic of a seal micro-leak or a propagating crack, and it should be treated as a structural failure rather than as a cosmetic defect. A spot that stays the same size across temperature cycles and time is more consistent with a trapped particle or a local cell irregularity, and it is a question of cosmetic acceptance.
The practical test is short: photograph the defect under a defined pattern, run a thermal cycle, and photograph it again at the same geometry. A change in size or shape moves the case from cosmetic to reliability.
Detection: dark-field, flat-field and magnification
Black spots are easiest to see where the eye expects uniformity.
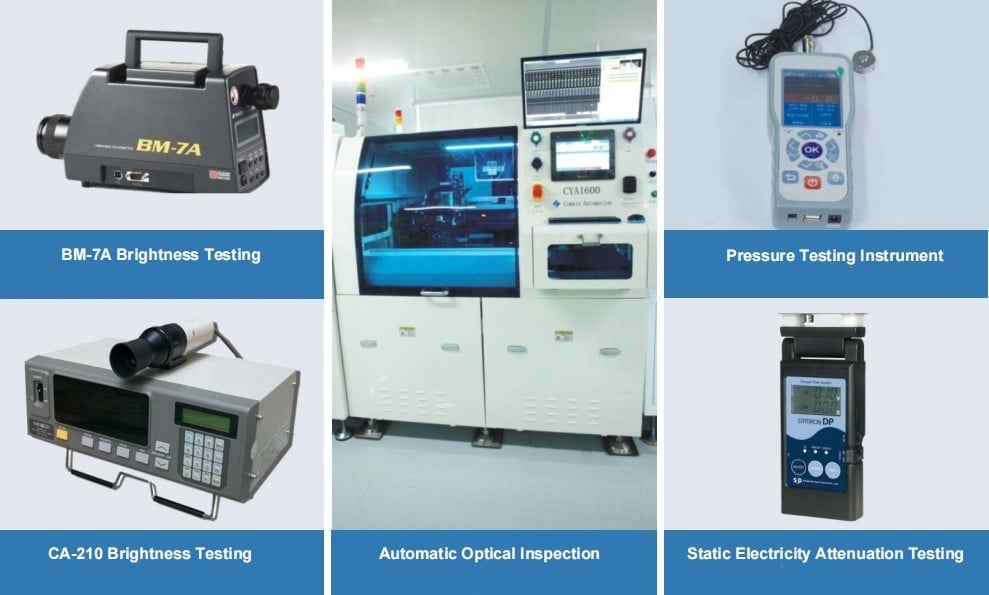
Inspection on a uniform white or grey field reveals area defects that photographic content hides; a dark-field view with the panel off isolates backlight contamination; and magnification with grazing illumination reveals particles and surface damage. Automated optical inspection, where it is available, adds repeatability because it applies the same illumination and threshold to every unit, which is what makes a cosmetic standard enforceable across shifts and sites.
CDTech’s notes on how AOI detects defects in LCD displays describe the imaging and threshold side of that inspection, and how AOI supports defect-free shipments covers what it takes to keep the process stable.
Pixel defect classes and where spot sizes fit
A black spot is not the same thing as a defective pixel.
Pixel defect standards – the ISO 9241-307 family is the one most often quoted in display supply – classify defective pixels by type and by the number permitted in a given class. A cluster of dead pixels can look like a black spot, but a continuous area defect usually falls outside the pixel-defect framework and belongs in the cosmetic acceptance standard instead. Mixing the two frameworks is a common source of disputes, because a buyer applies a pixel-class limit to a defect that is not a pixel at all.
Keep the two separate in the specification: one table for pixel defects by class, and one for area and cosmetic defects by size, zone and count. CDTech’s blog explains the pixel classification in ISO 9241-307 pixel defect classes for buyers and QC. Workmanship and inspection expectations for the assembly stages are published by bodies such as IPC.
Writing acceptance limits that a supplier can apply
Size, zone and count, with the viewing condition stated.
A workable acceptance limit names the defect size threshold, divides the active area into zones with different allowances (centre, general area, edge), states the maximum count per unit and per zone, and defines the viewing condition: distance, illumination, pattern and whether the display is powered. Where the application is a medical or inspection display, the limits tighten and the standard should say so explicitly rather than leaving it to interpretation.
Boundary samples – physical units or photographs agreed by both parties – turn those numbers into something an inspector can apply at the station. Without them, the same specification is interpreted differently at every site. Where an independent measurement is needed to settle a batch dispute, accredited laboratory scopes are published by organisations such as Intertek.
Incoming inspection and AQL treatment
Sample size and acceptance number should follow the consequence of a miss.
Where a black spot would stop a production line or trigger a field return, more inspection is justified; where it is cosmetic and the supplier’s process is stable, sampling is sufficient. The incoming check itself is short: power the unit, show a uniform white field, inspect the active area against the boundary samples, and record the defect category, size and zone rather than only pass or fail. Recording the category is what allows a trend to be seen across lots.
Rejected units should be preserved for the supplier’s analysis rather than scrapped locally, because the analysis needs the physical evidence. CDTech’s notes on what to test when LCDs arrive cover the receiving routine.
What a supplier should provide in a failure analysis
Mechanism, layer and corrective action – not a replacement credit.
A useful analysis states which layer the defect sits in, how that was determined, whether it is a production or field cause, and what process control changes. Where the defect is a seal micro-leak, the analysis should identify the seal process parameter that deviated. Where it is a particle, the analysis should identify the stage at which it entered the stack. That level of answer is only possible when the supplier controls the bonding and assembly steps, which is one argument for a supplier that manufactures display, touch and bonding in one flow.
Where a supplier cannot section the stack, ask for the incoming inspection records for the panel lot and the process records for the bonding run. Those two documents together usually locate the problem. Certificate scope can be checked through an accreditation register as described by the International Accreditation Forum.
Prevention: the controls that reduce incidence
Cleanliness, handling and load paths, in that order.
Particle-related spots fall with controlled assembly environment, ionisation at bonding stations, defined handling rules and periodic fixture cleaning. Cell and seal defects fall with panel-lot control and edge inspection before lamination, because a defect that is visible before bonding should never be bonded. Pressure-related spots fall with fixture design that distributes load, trays that do not press on the active area, and mounting designs that avoid point loads.
Traceability ties the three together: when a spot appears, the lot records should show which panels, adhesives and process runs were involved, and whether other units from the same combination are affected. CDTech’s quality system runs an inspection chain from incoming material through in-process, quality assurance, final, functional and visual checks to outgoing inspection, and its quality certifications page lists the certificates behind that flow. Measurement definitions for colour and appearance work are maintained by the CIE, and panel and defect trends are reported by research firms such as TrendForce.
When a black spot is a field problem rather than a supply problem
Field causes are mechanical and environmental, and they leave a signature.
Spots that appear after installation usually come from point loads in the mounting, impact damage, or ingress that reaches the cell edge. Their signature is a location that matches a mechanical feature – a screw boss, a clamp, a gasket corner – and a timing that follows an event rather than a lot. Comparing the defect map with the mechanical drawing answers this in minutes, and it prevents a supplier from being asked to fund a design problem.
Where the same failure appears across many units in different installations, the design is the cause; where it appears in one installation, the mounting is. CDTech’s notes on mura and luminance uniformity describe the related non-uniformity failures and how they are accepted.
FAQ
Can a black spot on a display be removed or repaired?
Not in any way that restores the panel. A black spot is a structural defect in the cell, the bond line or the backlight, and there is no field repair for it. The decision is whether it falls within the acceptance standard, and if it does not, the unit is rejected or replaced as a front assembly.
Why do some black spots grow over time?
Growth points to a breach in the edge seal or a propagating mechanical crack, where air or moisture enters and the damaged area extends. A spot that stays the same size and shape over thermal cycling is more consistent with a trapped particle or a local cell irregularity, and is treated as a cosmetic defect.
How do I tell a cell defect from backlight contamination?
Turn the display off. A backlight defect such as dust or a damaged diffuser is still visible as a dark region on an unpowered panel, while a cell defect or a pixel cluster is not. Viewing on a uniform white field and at several angles confirms the classification.
Do pixel defect standards cover black spots?
Only when the spot is made of defective pixels. The ISO 9241-307 pixel classes describe defective pixel counts and types; a continuous area defect is outside that framework and belongs in the cosmetic acceptance standard, which should specify size, zone and count limits separately.
What should be asked of a supplier after a batch shows black spots?
Ask for the failure analysis by layer: where in the stack the defect sits, how that was determined, whether the cause is production or field, and which process control changed. Incoming inspection records for the panel lot and process records for the bonding run usually locate the problem when sectioning is not available.
Next step
If a batch has shown black spots, send the defect map, the affected lot and photographs at a defined magnification to CDTech; the reply will classify the mechanism and state which process or design control applies.
Contact sales@cdtech-lcd.com or use the contact page; the technical resource centre is at display and touch solutions.
Related articles
 Second-Source Qualification for Display Modules Without Doubling Your Inventory RiskQuality, Testing & ComplianceIncoming Inspection for Display Modules: What to Check and How OftenQuality, Testing & ComplianceEMC Certification for Display Products: Passing the First TimeQuality, Testing & ComplianceScreen Damage Modes: Distinguishing Production Defects From Field DamageQuality, Testing & Compliance