How Do You Audit an LCD Factory?
An LCD factory audit is a logistics exercise as much as a technical one: plan the visit, agree the documents in advance, examine the right stations, and record findings in a form the supplier…
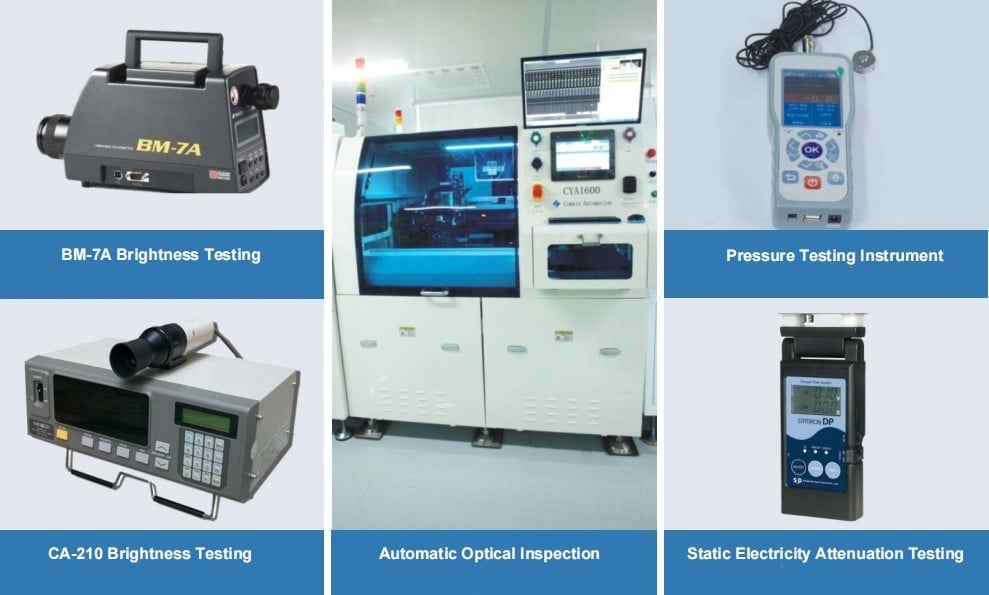
An LCD factory audit is a logistics exercise as much as a technical one: plan the visit, agree the documents in advance, examine the right stations, and record findings in a form the supplier can act on. This page covers that practical sequence. The evidence-based technique – following one unit through the plant and testing the traceability chain – plus red flags and follow-up, is in How to Audit a Display Factory: An Evidence-Based Checklist.
Part of the Custom Displays, Sourcing & Manufacturing guide — 81 articles on tooling, sampling, MOQ and supply-chain risk.
Before the visit
Request the process flow, control plan and inspection standard for the module you intend to buy, plus a recent reliability test report and the calibration list for the measuring equipment. Agree the audit scope: which lines, which processes and which product line. Bringing your own boundary samples for cosmetic acceptance turns the visit from a tour into a comparison.
Planning this way also shortens the visit, because the documents arrive before the discussion rather than during it.
The facility tour: what to look at
The areas worth the time are incoming material inspection, the cleanroom or bonding area if the module is bonded, final inspection with its illumination and viewing distance, and the packing area. In the bonding area, look at the environment and the process records for the running shift; at final inspection, compare a rejected unit and a passing unit against your boundary samples.
The tour is also the moment to look for the practical things: how parts are stored, how rework is handled, and whether the inspection station can actually apply the standard it claims.
Equipment and calibration
List the equipment that matters for your module – luminance meter, chambers, functional test rigs, AOI if present – and ask for the calibration records for each. Then ask a more revealing question: what the equipment is used for, and how often. Equipment that exists but is not calibrated, or a chamber that cannot achieve the profile in the specification, tells you more than an equipment list.
Where a measurement feeds a specification claim, the instrument’s calibration status is part of the claim.
Quality system and records
Ask for incoming inspection records for the panels, ICs, LEDs, adhesive and glass used in your module; the non-conformance log for the last months; and a worked example of traceability from a finished lot back to those materials. The records are what distinguish a certified factory from a controlled one.
CAPA records, with the containment, root cause and verification of effectiveness, show how the factory behaves when something goes wrong. Workmanship standards are published by bodies such as IPC, accreditation registers by the International Accreditation Forum, and environmental test scopes by laboratories such as Intertek.
On-site sample testing
Where the visit allows, take a unit from stock and test it against the specification: power-up, functional check, optical spot measurement and a cosmetic comparison against your samples. It is a small sample and it will not prove capability, but it does show whether the factory’s own inspection is finding what yours would find.
Recording the result in the same format as your own receiving inspection makes the comparison meaningful.
Where to go next
For the evidence-based walk-through, the red flags that should stop a qualification, how to audit outsourced processes and how to write and follow up the report, read How to Audit a Display Factory: An Evidence-Based Checklist. Related: which factory certifications matter.
FAQ
What should be requested before an LCD factory audit?
The process flow, control plan and inspection standard for your module, a recent reliability test report, the calibration list for the measuring equipment, and agreement on which lines and processes are in scope. Bring your own boundary samples so cosmetic acceptance can be compared on the spot.
What should be examined during the tour?
Incoming material inspection, the bonding or cleanroom area with the running shift’s process records, final inspection with its illumination and viewing distance, and packing. Compare a rejected and a passing unit against your boundary samples to see whether the same standard is being applied.
Does on-site sample testing prove capability?
No, but it shows whether the factory’s own inspection finds what yours would. Test a unit from stock against the specification in the same format as your receiving inspection, and record the result alongside the documents reviewed.
Next step
Send the module specification and the audit scope to CDTech; the reply will provide the process flow, inspection standard and records relevant to that scope.
Contact [email protected] or use the contact page.
Related articles
 Touch Screen Grounding: Debug Floating and Earth-Referenced Installations SeparatelyCustom Displays, Sourcing & ManufacturingCapacitive Touch Glove Thickness: Validate Material and Fit Before Setting SensitivityCustom Displays, Sourcing & ManufacturingCapacitive Touch Water Rejection: Distinguish Droplets, Films and Flowing WaterCustom Displays, Sourcing & ManufacturingCapacitive Touch Charger Noise: Correlate Raw Data with Power-Supply ConditionsCustom Displays, Sourcing & Manufacturing