Medical Display Supply Chain: Traceability and Change Control
A display module contains a panel made by one company, a driver IC from another, a backlight with LEDs from a third, an adhesive from a fourth and a cover glass from a fifth.…
A display module contains a panel made by one company, a driver IC from another, a backlight with LEDs from a third, an adhesive from a fourth and a cover glass from a fifth. Traceability in a medical device therefore has to cross several tiers, and the most common failure is not a missing record at the module level but an invisible change two tiers down that invalidates the manufacturer’s own validation.
Part of the Medical & Clinical Displays guide — 22 articles on DICOM, IEC 60601-1, hygiene and patient monitoring.
Why a display is a critical component in a regulated device
It carries information and it touches the patient’s environment.
In a regulated device, the display typically conveys values, alarms or images that clinicians act on, and its front surface sits in a cleaned environment. Both facts make it critical in the risk analysis: a change in luminance, colour, uniformity or response time can alter clinical interpretation, and a change in materials can affect cleaning performance or biocompatibility. That is why display changes require evaluation rather than substitution, even when the electrical specification is unchanged.
The practical consequence for procurement is that the display needs the same change-control discipline as any other critical component, with a documented rationale for every revision that reaches the device.
Traceability from panel lot to finished device
The chain must be reconstructable, not just documented.
A workable traceability chain links the finished device serial number to the display module lot, and the module lot to the panel lot, the LED bin, the bonding material batch and the cover glass batch. The test is whether a failure investigation can reconstruct that chain from records in a reasonable time, using only the device serial number as the starting point. A system that requires a phone call to a distributor does not meet that test.
Ask the supplier to demonstrate the reconstruction on a real example rather than describing the system. CDTech’s notes on medical display supply chain traceability and change control describe how this is maintained in a controlled medical display programme.
Change notification agreements and timelines
A PCN is only useful if it arrives before the change ships.
The purpose of a product change notification is to give the device manufacturer time to assess the impact, decide whether revalidation is needed, and update documentation. That requires a notification window measured in months for material changes, not days. The agreement should state the categories that trigger notification – panel source, driver IC, LED bin, adhesive, glass, coating, production site, firmware – and the response window on each side.
Equally important is the change that does not trigger notification: a process improvement that alters no characteristic. The supplier should be able to demonstrate that such changes are controlled internally and that the verification data supports the claim. Quality-system practice for these agreements is described through bodies such as IAF-accredited certification frameworks, and general quality resources are maintained by organisations such as ASQ.
Panel manufacturer discontinuation risk
The display supplier does not control the panel roadmap.
Panel makers discontinue generations on their own schedule, and a module manufacturer’s ability to continue supply depends on its stock position and on the availability of a qualified alternative. That risk is best managed before it materialises: ask the supplier which panel each module uses, what its own visibility is on discontinuation, and what the plan is for a replacement, including the interchangeability level and the validation it would require.
Where volume justifies it, a last-time buy sized for production plus service is the practical mitigation; where it does not, a pre-qualified alternative module is the cheaper option.
Supplier audits: what evidence proves control
Audit the records that the process produces, not the processes that are described.
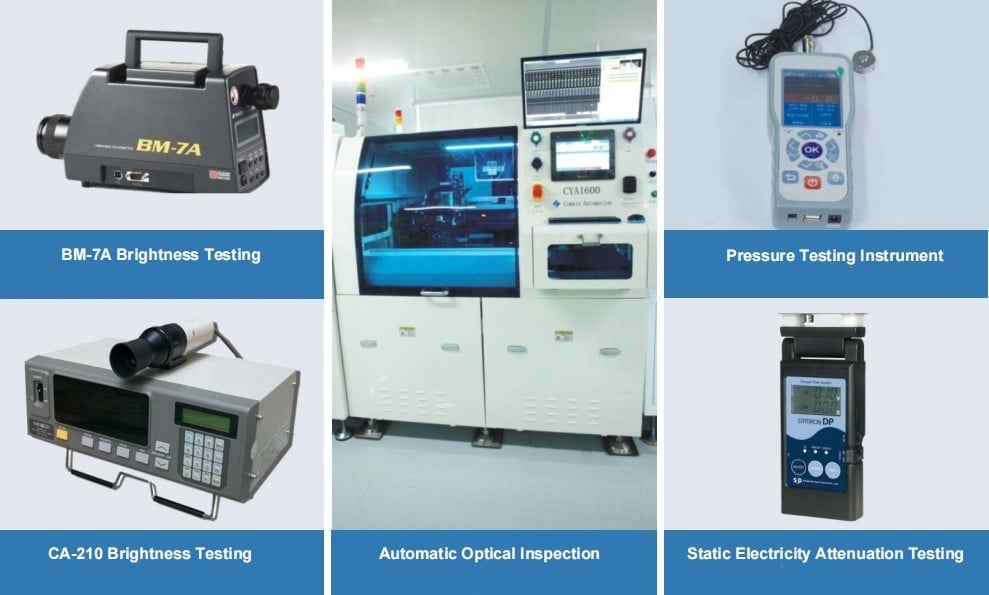
A display supplier audit should follow one physical module through incoming inspection, assembly, bonding, final test and packing, asking for the record at each stage. The evidence that proves control is consistent and complete: incoming material records with lot numbers, process parameter logs for bonding and lamination, test results with limits and pass/fail, and a non-conformance record for anything that was reworked. Where a process has no measurable parameter – a visual inspection, for example – the acceptance criteria should exist as a document with photographs or boundary samples.
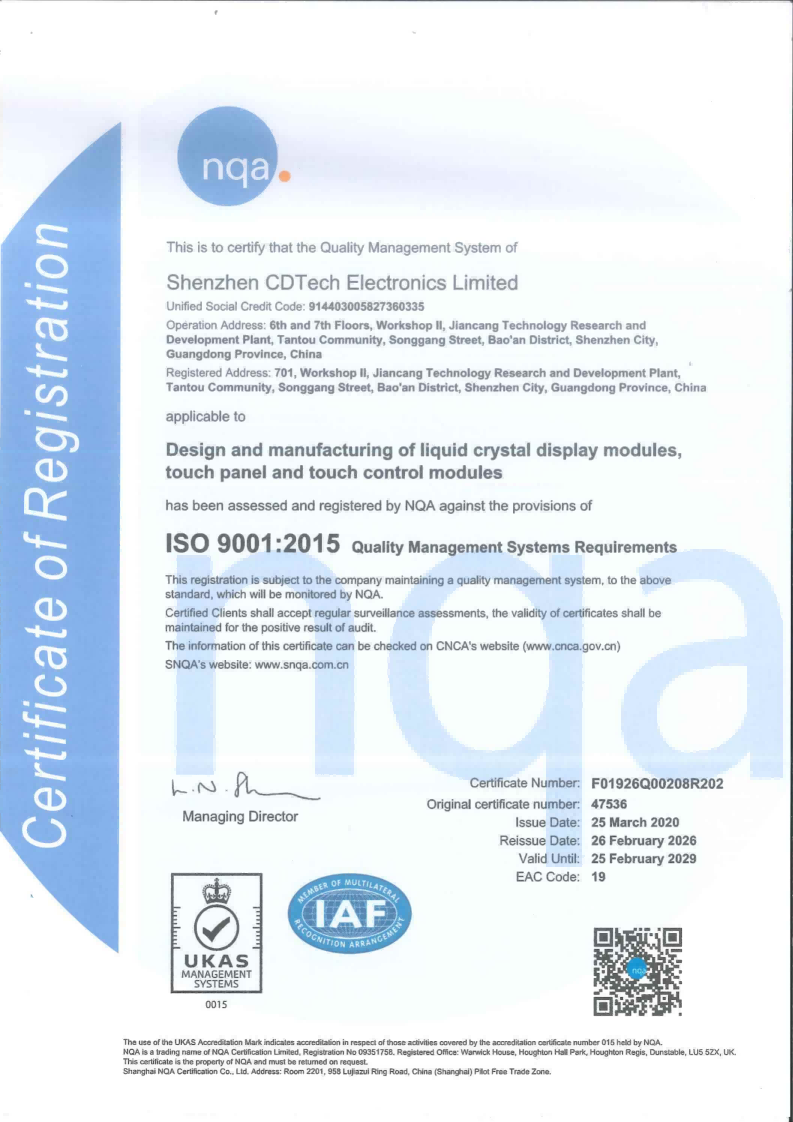
CDTech’s quality chain of incoming, in-process, quality assurance, final, functional and visual checks before outgoing inspection maps directly onto that audit path, and the quality system scope is published on the certifications page.
Sub-supplier visibility and second-tier risk
The risk that matters most is the one nobody reports.
Module manufacturers buy panels, ICs, LEDs, adhesives and glass from other companies, and some of those suppliers change their own materials. A practical agreement requires the module supplier to flow down the notification obligation to sub-suppliers for the materials critical to the device, and to name which materials those are. Bonding adhesive and cover glass coating are usually on that list, because a change there affects optical and cleaning performance with no electrical signature.
Ask for the critical sub-supplier list with the notification arrangements for each. If the list does not exist, the change-control agreement has a hole in it.
Non-conformance handling and CAPA expectations
The response to a failure is the best evidence of the system.
For a medical component, the expectation is a documented non-conformance record, a containment action, a root-cause analysis and a corrective action with verification of effectiveness – the standard CAPA cycle. The practical questions in a supply agreement are the acknowledgement time, the containment time and the analysis deadline, plus the requirement to preserve failed parts for investigation rather than scrapping them.
Traceability and CAPA work together: root-cause analysis is only possible if the affected material lots can be identified and their fate determined across finished devices.
Storage, shelf life and re-qualification rules
Aged stock is a compliance question as well as a technical one.
Displays stored for years can experience polarizer edge lift, adhesive creep and connector oxidation, and a device built with aged stock may behave differently from one built with fresh material. A workable rule is to define a shelf life for the module, require storage conditions to be recorded, and specify a re-qualification test for stock beyond the shelf life – sampling across pallets and storage positions, and checking optical, functional and adhesion behaviour rather than power-on alone.
Packaging and handling requirements for electronic assemblies are published by bodies such as IPC, and component lifecycle management practice in distribution is visible through sources such as Mouser.
Business continuity planning with a display supplier
Continuity is a set of agreements, not a document.
Effective continuity planning for a display supply covers four things: a second source that is qualified and periodically built, a defined minimum stock level for critical parts, a documented response to a production interruption at the supplier, and a plan for the tooling if it is owned by the customer. Each of these is testable, and each should have an owner and a review date.
The most commonly missing element is the annual build of the second source: a second source that has not been exercised in two years is a drawing, not a supply option.
Contract clauses that protect device certification
Five clauses do most of the work.
- Notification of defined change categories within a stated period before shipment.
- Flow-down of notification obligations to critical sub-suppliers, with the list named.
- Traceability records retained for a defined period and produced on request.
- Non-conformance and CAPA timing commitments, with failed parts preserved.
- Discontinuation notice with a last order date sufficient for a last-time buy.
These clauses cost nothing to negotiate at the start of a programme and are effectively unobtainable once a device is in the field. Accreditation frameworks such as those maintained by IAF and laboratory accreditation through ILAC provide the context for verifying that a supplier’s certificates are genuine and in scope.
FAQ
What is a PCN in display supply?
A product change notification: a formal notice that a supplier will change a part, process, material or production site. For medical devices it should arrive well before the change ships, name the affected part numbers and categories, and state whether form, fit, function or regulatory characteristics are affected.
How should a medical device maker audit a display supplier?
Follow one module through the production flow and ask for the record at each stage: incoming material lots, process parameters, test results with limits, and non-conformance handling. Then test the traceability chain by reconstructing a finished device’s module history from its serial number.
How do I manage second-tier supplier risk?
Require the module supplier to list the sub-suppliers whose materials are critical to your device – panels, driver ICs, LEDs, adhesives, glass and coatings – and to flow the notification obligation down to them. Verify that list exists; without it, changes can occur two tiers down with no visibility.
Does stored display stock expire?
It degrades, and the rate depends on packaging and storage conditions. Define a shelf life, record the storage environment, and re-qualify stock beyond that period by sampling across pallets and positions and checking optical, functional and adhesion behaviour rather than power-on alone.
Next step
Send the device classification, critical characteristics and audit requirements to CDTech; the reply will provide the traceability example, change notification commitment and quality records relevant to your programme.
Contact [email protected] or use the contact page.
Related articles
 Ventilator and Infusion Pump Displays: Design ConstraintsMedical & Clinical Displays
 Patient Monitor Displays: Specs, Interfaces, and CertificationsMedical & Clinical Displays
 Custom Medical Displays: DICOM, Grayscale, and Panel SelectionMedical & Clinical DisplaysDental, Ophthalmic and Aesthetic Device Displays: Colour and Detail Under MagnificationMedical & Clinical Displays