How to Audit a Display Factory: An Evidence-Based Checklist
Differentiation page: publish the linked new page before the foundation rewrite of the old page. | Meta description: How to audit a display factory: the evidence that proves control, what to watch for on…

A display factory audit succeeds or fails on one technique: following a physical unit through the process and asking for the record it produced at each step. Presentations describe systems; records show whether the systems operate. An auditor who spends the day with documents and an afternoon on the line usually learns less than one who does the reverse.
Part of the Custom Displays, Sourcing & Manufacturing guide — 46 articles on tooling, sampling, MOQ and supply-chain risk.
Prepare with the specification in hand
Audit against your own part, not a generic checklist.
Before arriving, obtain the control plan, the inspection standard and the process flow for the specific module. The audit then verifies whether those documents describe what happens on the line, and whether the records exist to prove it. Generic audits produce generic findings; auditing your own part produces findings that affect your product.
Bring the boundary samples agreed for cosmetic acceptance, and use them on the line to see whether the inspectors apply the same standard you will apply at receiving.
Start with incoming materials
The first process determines much of the quality.
Ask for the incoming inspection records for the panels, the driver ICs, the LEDs, the adhesive and the cover glass used in your module. Then ask how a non-conforming lot is handled: where it is stored, who authorises disposition, and what the record looks like. A factory that cannot show a rejected lot’s record is not performing incoming inspection in a way that affects production.
The related question is traceability: can the panels in front of you be linked to their incoming records by lot number? If not, the traceability chain in the finished product is unlikely to be complete.
The bonding and assembly area
Process control is visible in the room.
Where bonding takes place, the audit should examine the environment – cleanliness, humidity control, ESD measures – and the process – adhesive handling, defoaming or vacuum steps, cure profile and the inspection that follows. Ask to see the parameter records for the shift that is running, and compare them with the limits in the process specification. Second, look at the inspection: bonding defects are judged against criteria, and the criteria should be displayed or documented rather than held in an inspector’s memory.
Where the process is manual, look at how the operator knows the limits, and whether the fixture enforces them.
Final inspection and the cosmetic standard
Appearance is where most disputes originate.
Ask to see the final inspection station, the illumination used, the viewing distance and the defect standards. Then take a unit that was rejected and a unit that passed, and compare them with your boundary samples. Where the factory’s standard is looser than yours, no amount of downstream negotiation will fix it, and the time to discover that is during the audit rather than at receiving.
The related check is whether the inspection results are recorded per unit or per lot, and whether the records distinguish defect categories. A count of rejects without categories cannot be analysed later.
Testing, reliability and calibration
Equipment that is not calibrated is not testing anything.
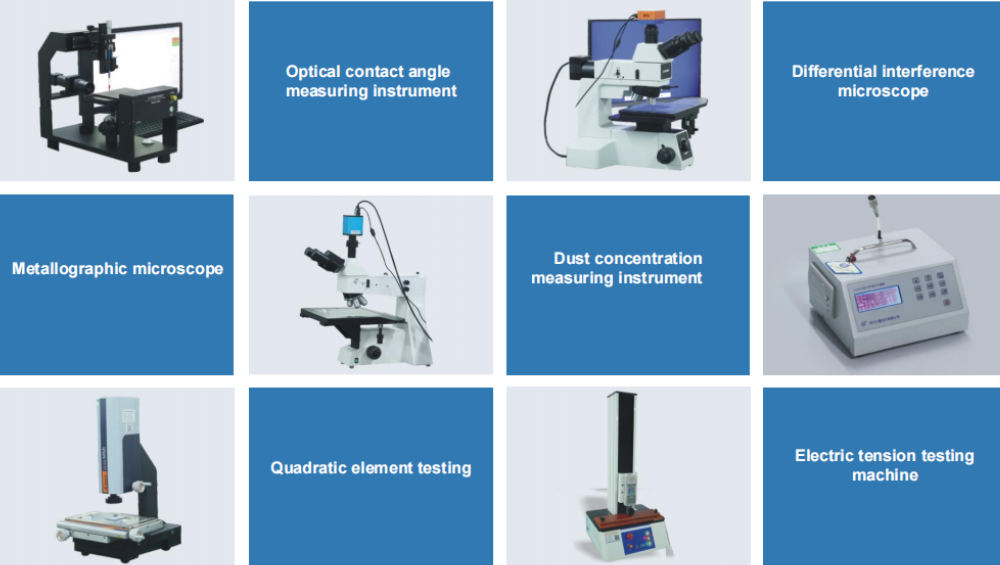
Ask for the calibration records for the luminance meter, the power supplies, the temperature chambers and any measuring instruments. Then ask how the reliability tests are scheduled and whether the results are retained per lot or only per product family. Where the factory performs thermal, vibration or aging tests, examine a recent report against the profile in the specification, including the ramp rates and dwell times.
A common finding is equipment that is present but not calibrated, or a chamber that cannot achieve the specified ramp rate. Both are more informative than the equipment list.
Traceability, change control and documentation
Follow one unit’s history.
| Stage | Record to request |
|---|---|
| Incoming inspection | Lot records for panel, IC, LED, adhesive, glass |
| Assembly and bonding | Process parameters and operator identification |
| Testing | Functional and optical results with limits |
| Non-conformance | Rejection record, disposition and authorisation |
| Packing and shipping | Lot identity, packaging specification, ship record |
The purpose is to reconstruct the history of a specific unit within an hour. Where that is not possible, the traceability claim in the quality documentation is weaker than it appears.
Red flags that justify ending an audit early
Five findings that stop a qualification.
- Certificate scope that excludes the site or product line being audited.
- No traceability from finished goods back to the material lots.
- Inspectors applying a cosmetic standard looser than the agreed one.
- Measuring equipment out of calibration, or no calibration records at all.
- Process parameters outside the documented limits on the running shift.
Each of these affects product shipped tomorrow, which is why they take precedence over improvements that could be made over time. An audit report that records them with photographs and document references is more useful than a score with no evidence.
Auditing processes that are outsourced
The boundary of the audit should match the boundary of the product.
If the cover glass coating, the FPC or the bonding is performed by a third party, the audit should either visit that site or examine the controls the module supplier applies to it. The relevant questions are whether the sub-supplier is on a controlled list, whether incoming inspection is performed on their deliveries, and whether changes at that site are notified. A module supplier that cannot describe its sub-supplier controls has a gap in the same place as the process.
Where a visit is impractical, requesting the sub-supplier’s process records for the relevant lots is a reasonable substitute.
Writing the audit report
Findings, evidence and consequence.
- State the scope: site, product line, processes examined, date.
- Record each finding with the document reference or photograph that supports it.
- Classify findings by whether they affect shipped product or are improvement opportunities.
- Note the corrective action agreed and the date for re-verification.
- Record what was examined and found satisfactory, so the report shows the audit’s coverage.
A report structured this way supports a qualification decision and a follow-up visit. Workmanship and inspection standards referenced during the audit are published by bodies such as IPC, and protection practice for handling sensitive assemblies by the EOS/ESD Association.
Following up
The audit’s value is in the closure.
Where findings were raised, the supplier should return a corrective action with evidence, and the audit should confirm the effect on a later visit or through shipment data. Findings that are closed on paper and not re-verified are the most common reason an audit’s conclusions do not hold a year later. Scheduling the follow-up at the time of the original report, rather than when the next issue arises, keeps the process honest.
For programmes with a long life, repeating the audit periodically – with a narrower scope each time – maintains the picture without the cost of a full audit every year. CDTech’s notes on the same subject, and its published certification scope, illustrate the evidence set a display factory can provide.
FAQ
What should a display factory audit cover?
Incoming material records, the bonding and assembly process and its parameters, final inspection with its illumination and cosmetic standard, calibration of measuring equipment, reliability test records, traceability from finished goods to material lots, and change control. Follow the specific module you intend to buy through each stage.
What is the most useful audit technique?
Following one physical unit through the plant and asking for the record it produced at each step, then reconstructing its history from the finished-goods identity. Presentations and document sets describe systems; the records show whether those systems operate.
Which findings should stop a qualification?
Certificate scope excluding the audited site or product line, no traceability from finished goods to material lots, inspectors applying a looser cosmetic standard than agreed, measuring equipment out of calibration, and process parameters outside documented limits on the running shift. Each affects product shipped immediately.
How should audit findings be followed up?
With a corrective action backed by evidence and a re-verification through a later visit or shipment data. Findings closed on paper without verification are why audit conclusions stop being valid a year later; schedule the follow-up when the report is issued.
Next step
Send the module specification and the audit scope you intend to use to CDTech; the reply will provide the process flow, inspection standard, calibration and traceability records relevant to that scope.
Contact sales@cdtech-lcd.com or use the contact page.
Related articles
 Fuel Dispenser and Forecourt Displays: Safety, Sunlight and Continuous UseCustom Displays, Sourcing & Manufacturing
 Landed Cost for Display Modules: Freight, Duty, Packaging and the True Unit PriceCustom Displays, Sourcing & Manufacturing
 TFT LCD vs OLED vs E-Paper for Industrial Products: A 2026 Decision FrameworkCustom Displays, Sourcing & Manufacturing
 Segmented and Memory LCDs: Low-Power Alternatives Buyers Keep OverlookingCustom Displays, Sourcing & Manufacturing