Inspecting Optical Bonding Quality in Display Modules
Optical bonding improves contrast and reduces internal reflections, and it introduces a class of defects that exist between two layers and cannot be repaired by tightening a screw. Inspecting the result is a skill…

Optical bonding improves contrast and reduces internal reflections, and it introduces a class of defects that exist between two layers and cannot be repaired by tightening a screw. Inspecting the result is a skill with a method: the conditions determine what you see, and the acceptance logic determines what you do about it.
This article covers how to inspect bonded assemblies consistently and how to record findings so that a claim is accepted rather than argued.
Inspection conditions that change what you see
The same assembly inspected under different conditions produces different findings. Ambient light, viewing angle and the content displayed behind the glass each change which artefacts are visible.
Three conditions matter most. Reflected light – a lamp or window reflected in the surface – makes surface scratches and coating marks visible. Transmitted light – the panel displaying a white field – makes internal artefacts such as particles and voids visible. And raking light at a shallow angle makes delamination and edge effects visible along the boundary between layers.
An inspection that uses only one condition will miss two of the three artefact families. Recording the condition with each finding is what makes the result reproducible by someone else, including the supplier’s own quality engineer.
Artefact classes and how they appear
Bonding defects fall into a small number of families, each with a characteristic appearance.
| Artefact | Appearance | Usual origin |
|---|---|---|
| Particle | Small dark or bright spot, sharp edges, fixed under transmitted light | Contamination before or during lamination |
| Bubble or void | Rounded spot or crescent, may move slightly with temperature | Trapped air or incomplete adhesive flow |
| Delamination | Edge-origin region with a visible boundary, often growing from one corner | Adhesion loss from stress, contamination or cure issues |
| Adhesive unevenness | Broad soft patches, often near the middle or aligned with a feature | Thickness variation or flow marks |
| Edge seal void | Light band along the border, visible at a shallow angle | Incomplete fill at the perimeter |
The family matters more than the count, because each has a different consequence: a particle is a cosmetic issue with a permanent location, a void may change with temperature, and delamination implies an adhesion problem that will get worse.
Tools and viewing angles
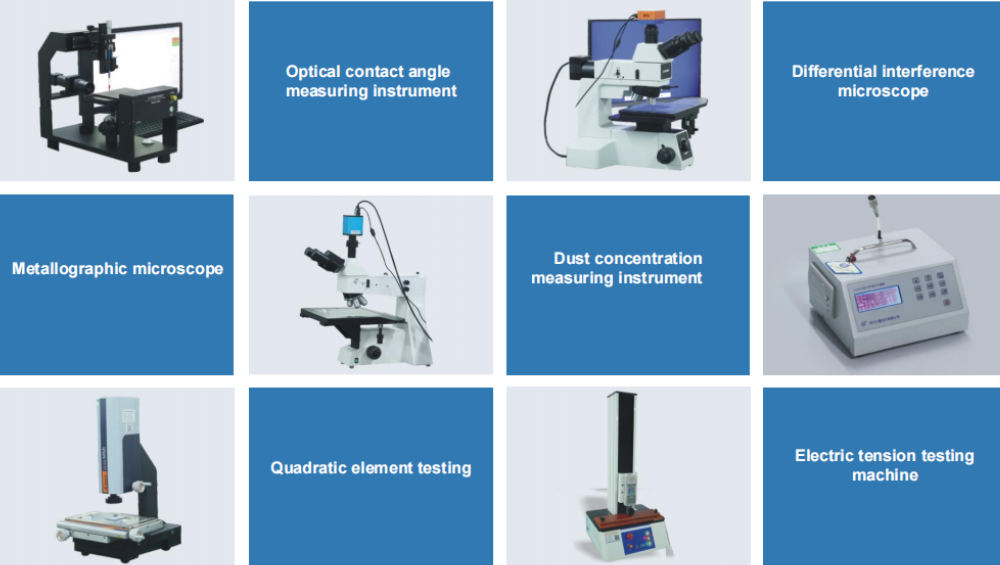
Most bonding inspection is visual, and the tools that help are simple: a controlled light source, a means of holding the assembly at a repeatable angle, and magnification for classifying small artefacts.
The angle matters because internal reflections change with it. An artefact that is invisible at normal incidence may be prominent at 30 degrees, particularly for edge voids and delamination. Where the product’s users will view the display at an angle – a tilted panel, a kiosk viewed from standing height – inspect at that angle rather than only head-on.
Keep the light source and the viewing position fixed between inspections. A finding that cannot be reproduced in the same conditions is difficult to defend, even when it is real.
Size, location and acceptance logic
Acceptance is best expressed as a rule combining size, location and count, rather than a single size limit. A small particle in the centre of the active area is more visible than a larger one near the edge; a void in a corner may never be noticed, while the same void on a medical image is unacceptable.
A workable rule states separate limits for the central zone and the border, a maximum size that is always rejected regardless of position, and a count limit within the central zone. The zones should follow the way the product is used: a screen where the operator reads values has a central zone that dominates the experience.
Cosmetic versus functional defects
The distinction is worth writing into the specification rather than leaving to the inspector. A simple table of artefact class against consequence – cosmetic only, affects touch, affects legibility – means two inspectors reach the same disposition, and it gives the supplier a rule to build to instead of an opinion to argue with.
Most bonding artefacts are cosmetic, but two families can become functional. A void or delamination in front of a touch sensor can change the coupling and produce a dead or noisy region. An artefact over a critical display area can reduce legibility in the same way as a bright defect in the panel.
The test is whether the artefact affects what the user does rather than how the product looks. That distinction should be explicit in the acceptance rule, because a defect that is cosmetic in one product is functional in another.
Ageing and thermal-cycling effects
The reliability tests that reveal growth are the ones described in thermal cycling and humidity testing, which set out the cycle counts and dwell times that make an effect visible. Not every artefact is present when the unit is new. Voids can grow or shrink with temperature, and delamination can progress from an edge over months of thermal cycling. An assembly that passes at room temperature may fail after a few dozen cycles.
Where the product experiences temperature extremes, the inspection should include the assembly after cycling. Recording the artefact’s condition before and after gives a growth rate, which is far more useful than a single observation: a small void that is stable is a different risk from one that doubles in size in a week.
Documenting findings for a claim
A claim needs evidence that the artefact is in the bonded interface rather than on the glass, and that the inspection conditions were consistent. Record the assembly serial, the conditions used, the artefact’s position as coordinates or a marked image, its measured size, and the acceptance rule it breaches.
Where the artefact is subtle, an image taken with transmitted light behind the panel plus one with reflected light on the surface usually settles whether it is internal or external. That pair of images is the most persuasive evidence available without destructive analysis.
Rework limits and consequences
Rework also changes the traceability picture. A reworked unit is not equivalent to a new one, and if the rework is not recorded, its later behaviour cannot be compared with the rest of the lot. Where rework happens, note it against the assembly identifier, along with what was separated and re-bonded.
Bonded assemblies can sometimes be separated and re-bonded, and the process has limits. Heating and separating a bonded stack risks stressing the panel and the cover glass, and each attempt reduces the yield of the next. Many suppliers specify a maximum number of rework attempts, and some do not accept reworked units as new.
Ask about rework policy before ordering, especially for a product where early units are likely to be reworked during development. A design that assumes rework is available may find that the units which come back are no longer within the optical specification.
Talking to the supplier with evidence
Where a dispute cannot be resolved on the record alone, a joint inspection is often faster than correspondence. Both parties measure the same unit, with the same conditions, and the disagreement usually narrows to a single number rather than a general claim – at which point the specification can be clarified so the same discussion does not return with the next shipment.
The conversation goes faster when the finding is expressed in the supplier’s own terms: the artefact family, its position, its size, the conditions under which it is visible, and the acceptance rule from the specification. Sending a photograph with no conditions usually leads to a request to return the unit for evaluation; sending the record above usually leads to a disposition decision.
Where the finding is at the boundary of the rule, agree the interpretation rather than arguing the individual part. A specification that is clear about zone limits avoids repeating the same discussion on every shipment. The construction choices behind the process are covered in the OCA versus OCR comparison.
Inspection record template
| Field | What to record |
|---|---|
| Assembly identifier | Serial, lot and date of manufacture |
| Conditions | Light source, angle, content displayed, magnification |
| Artefact class | Particle, void, delamination, unevenness, edge void |
| Position and size | Coordinates or marked image, measured dimension |
| Rule applied | The acceptance criterion and the zone it falls in |
| History | Inspected new, after cycling, or after service |
| Disposition | Accept, reject, rework or escalate |
If a bonding issue keeps appearing in the same position or the same production period, send us the record and the lot information – the pattern usually identifies whether the cause is contamination, process or handling.
Frequently asked questions
Is a bubble in the bonding always a defect?
It is an artefact whose acceptance depends on its size, position and whether it changes with temperature. The specification should define the limit rather than leaving it to judgement.
Can a bonded assembly be repaired?
Sometimes, by separating and re-bonding, but the process stresses the panel and reduces yield. Check the supplier’s rework policy and limits before relying on it.
Should bonding inspection happen before or after assembly into the product?
Both have value. Inspect the bonded module to isolate bonding issues, and inspect the finished product because that is the state the customer sees.